Parts machined to your print.
Specializing in titanium, tool steels, and other exotic materials.
Prototypes to low-volume runs, with the certs and paperwork your PO asks for.
Capabilities
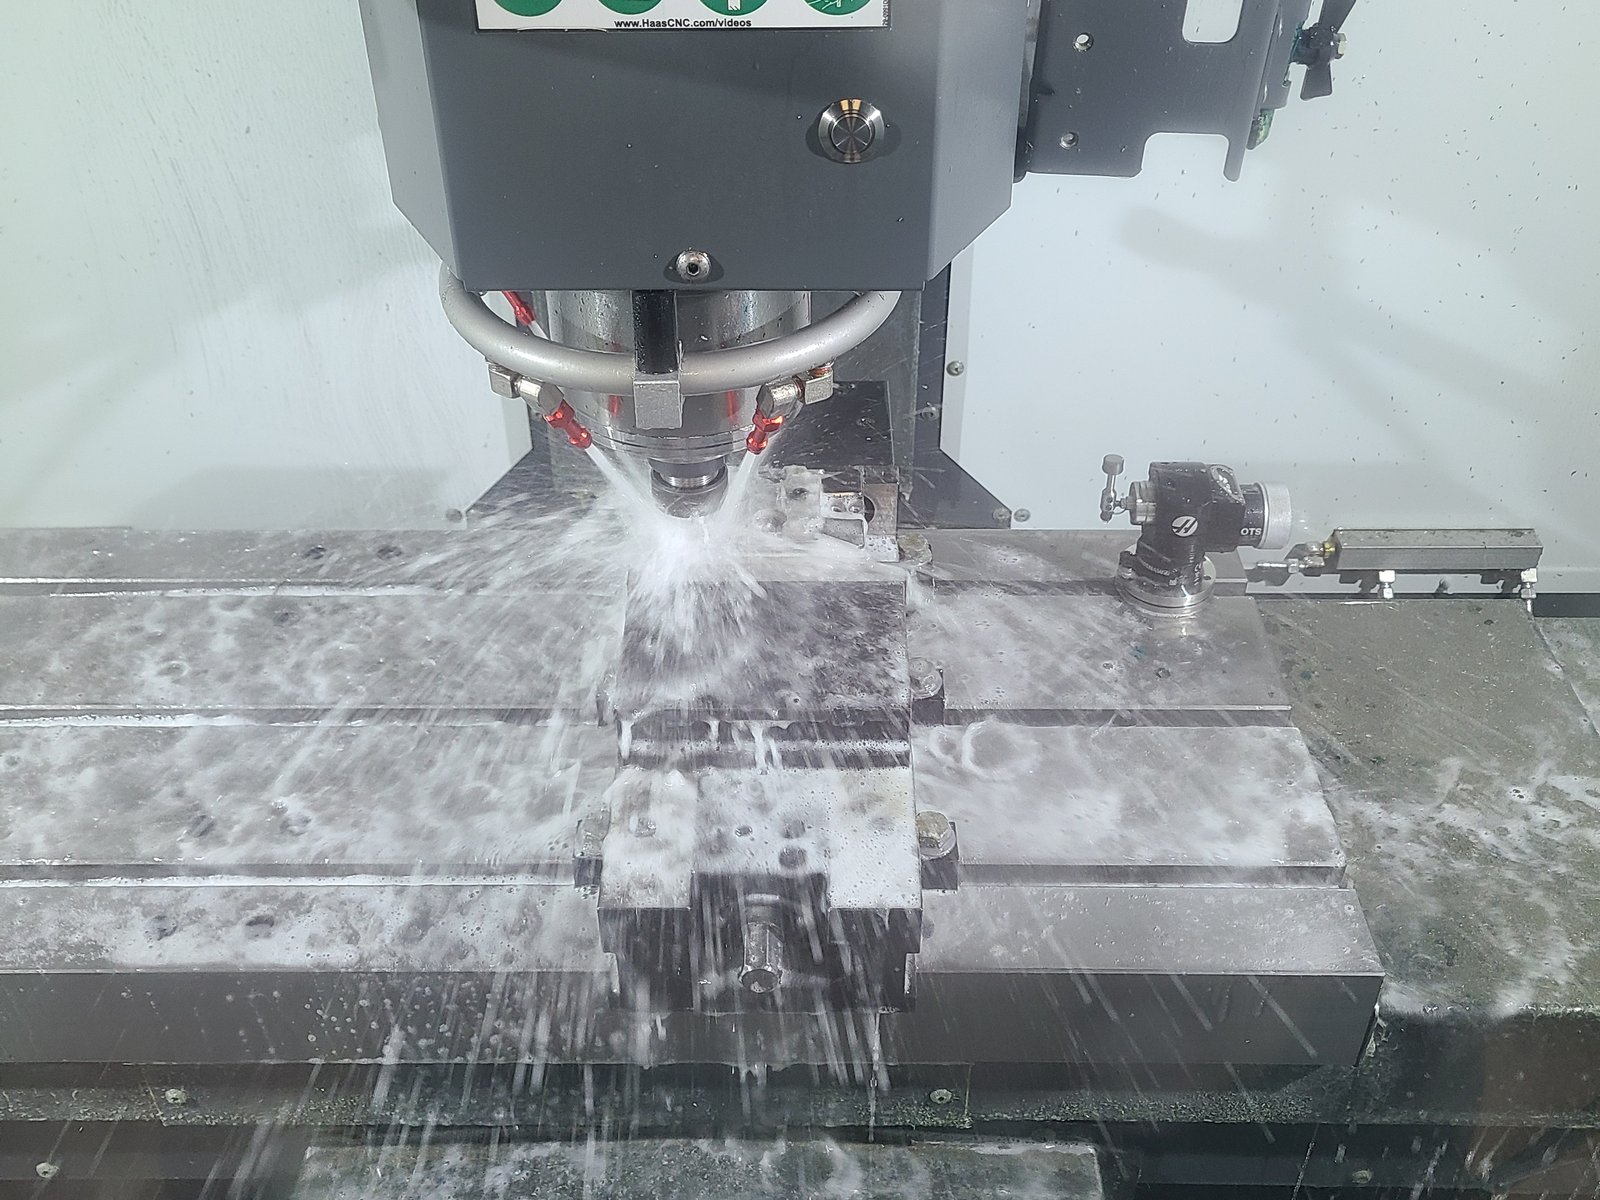
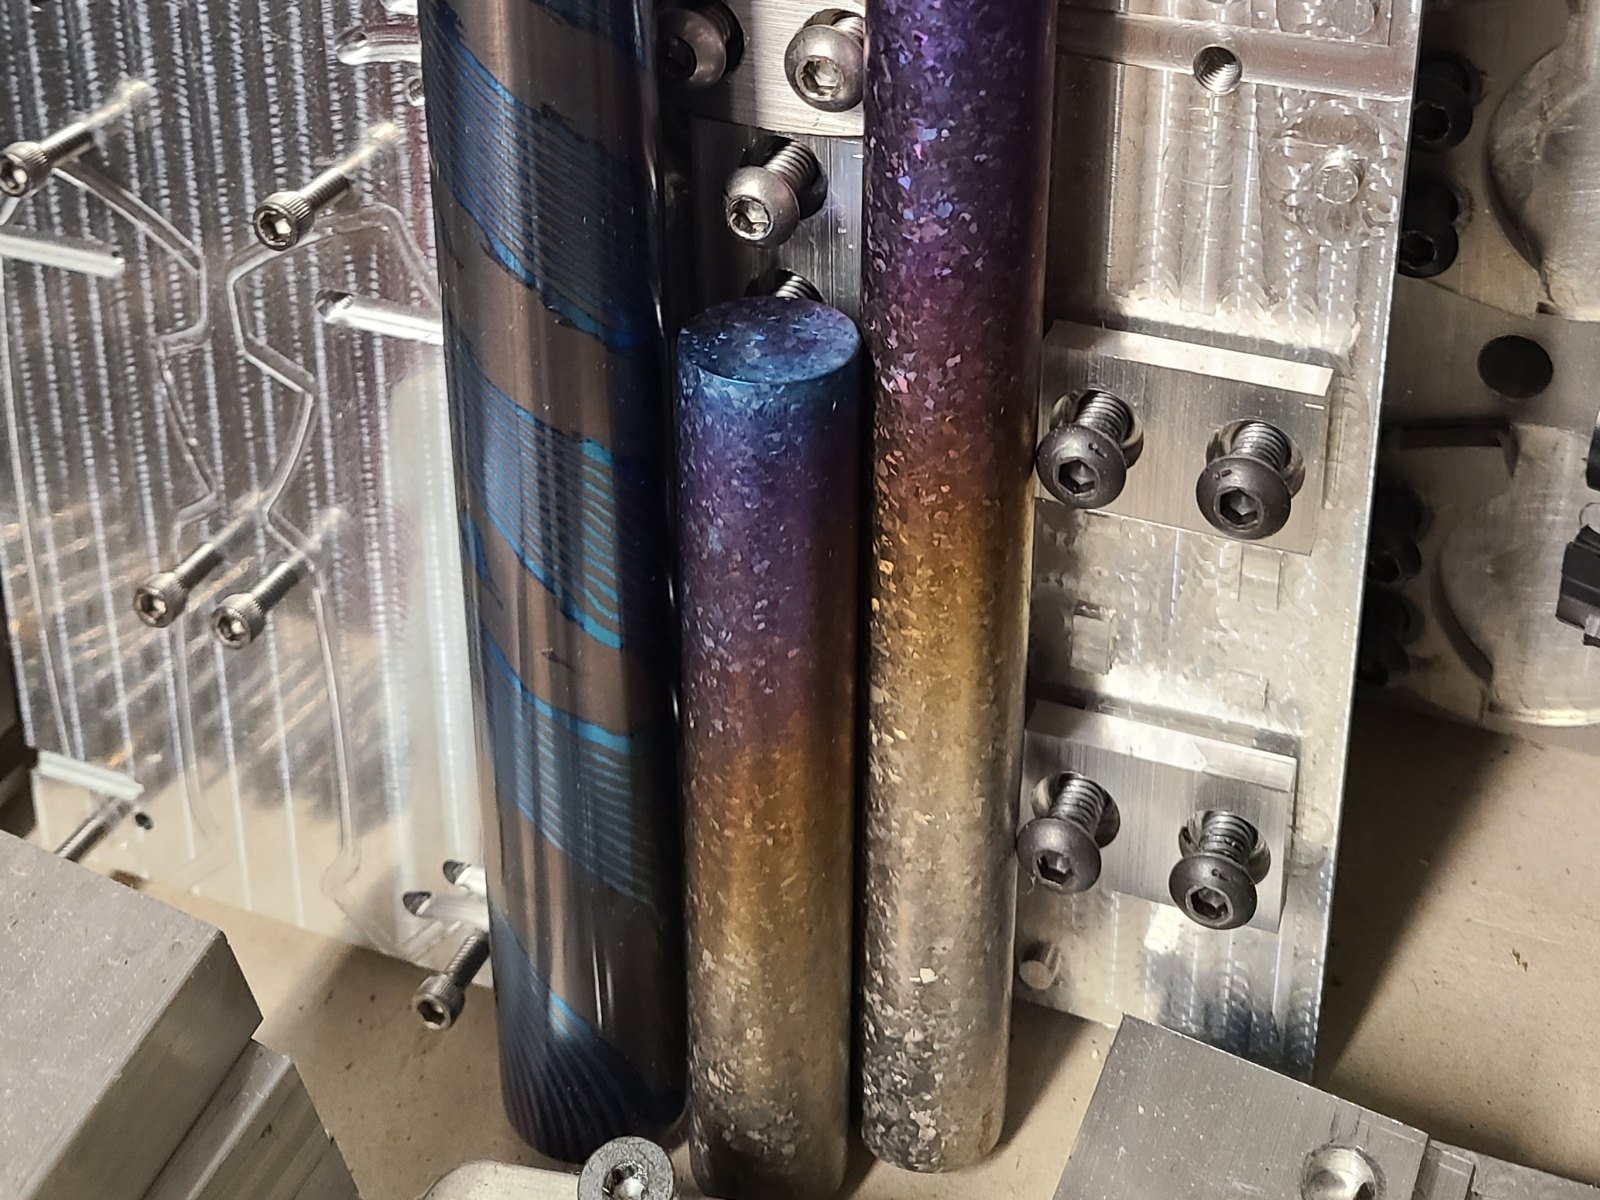
- Precision CNC machining in a wide variety of materials, many that other shops won’t touch.
- Custom fixturing built in-house so small parts and odd shapes run repeatably.
- Mechanical assembly, including rotating assemblies, mechanisms, and electrical, pneumatic, and hydraulic systems.
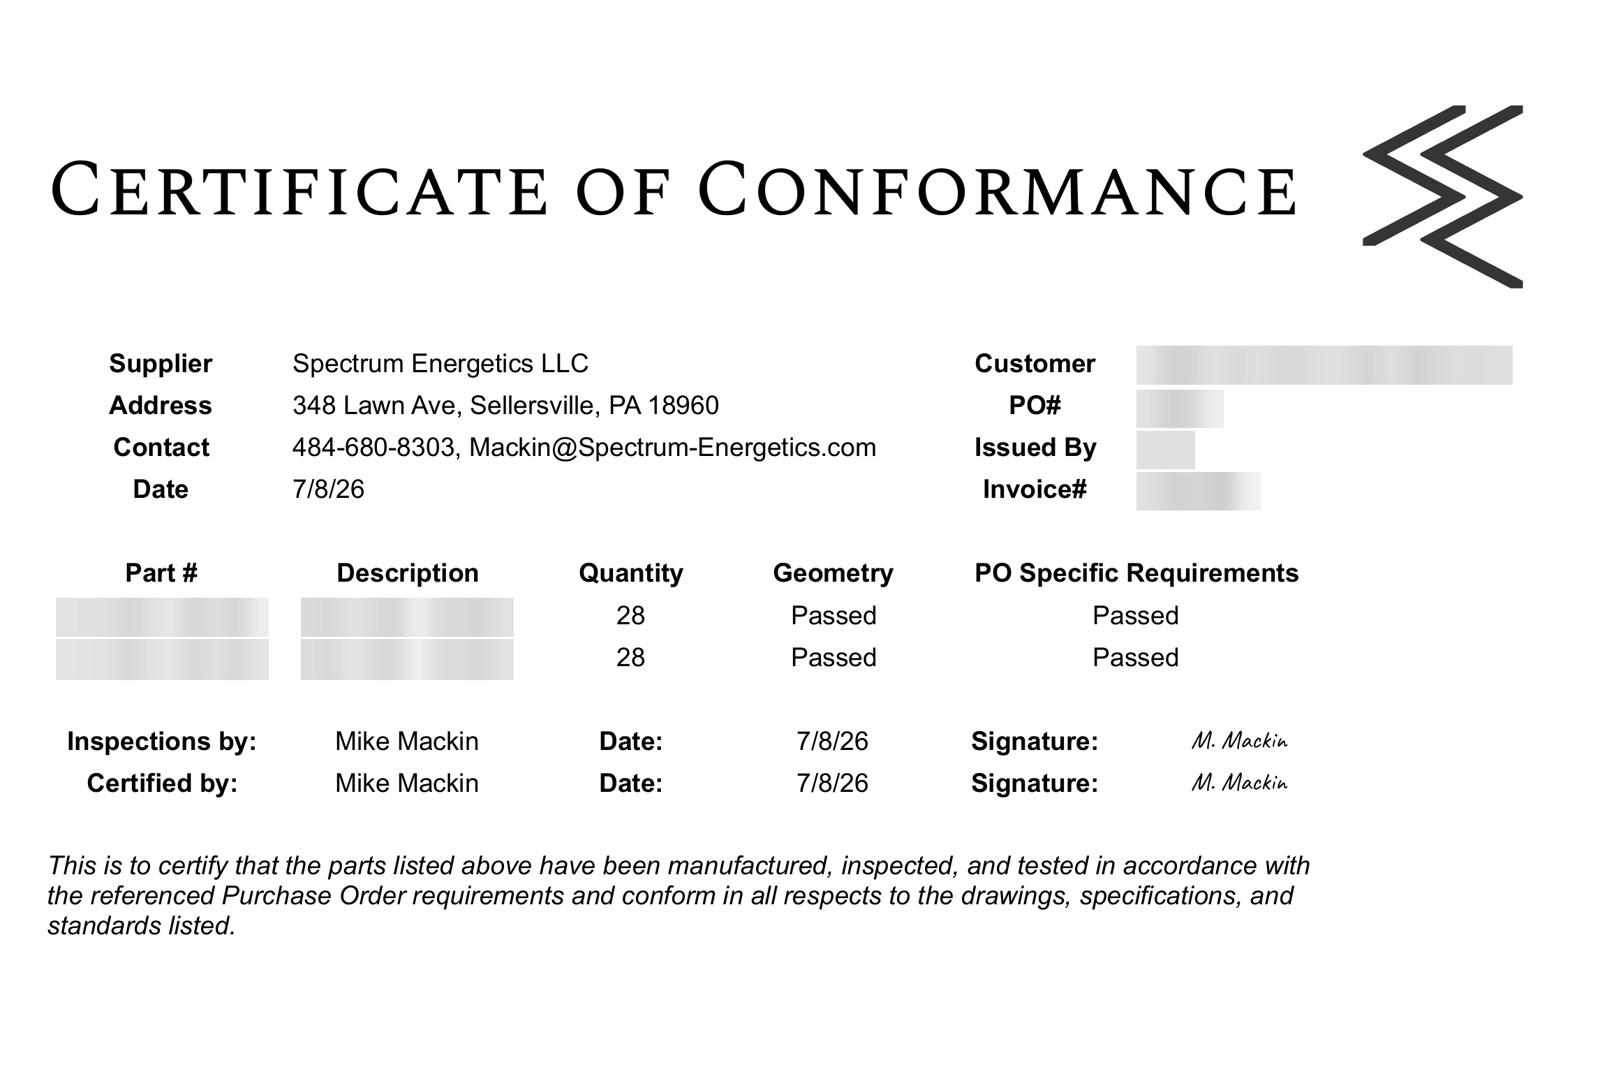
- Quality control: material certs, Certificates of Conformance, and inspection docs on request.
- Functional and aesthetic finishing, in-house and through partner shops.
Features from recent jobs
- 0.070" radius O-ring seats in the OD of Ø1.68" 316L stainless parts, cut with undercutting form tools on a 3-axis mill.
- Keyseats and slots, e.g. 1/8" wide by 0.108" deep in 303 stainless.
- Undercuts, internal radius grooves, back chamfers, and 140° chamfers.
- Small tapped holes (2-56 UNC) with counterbores and far-side thread reliefs.
- Engraved heat numbers for material traceability.
Equipment and processes
In-house
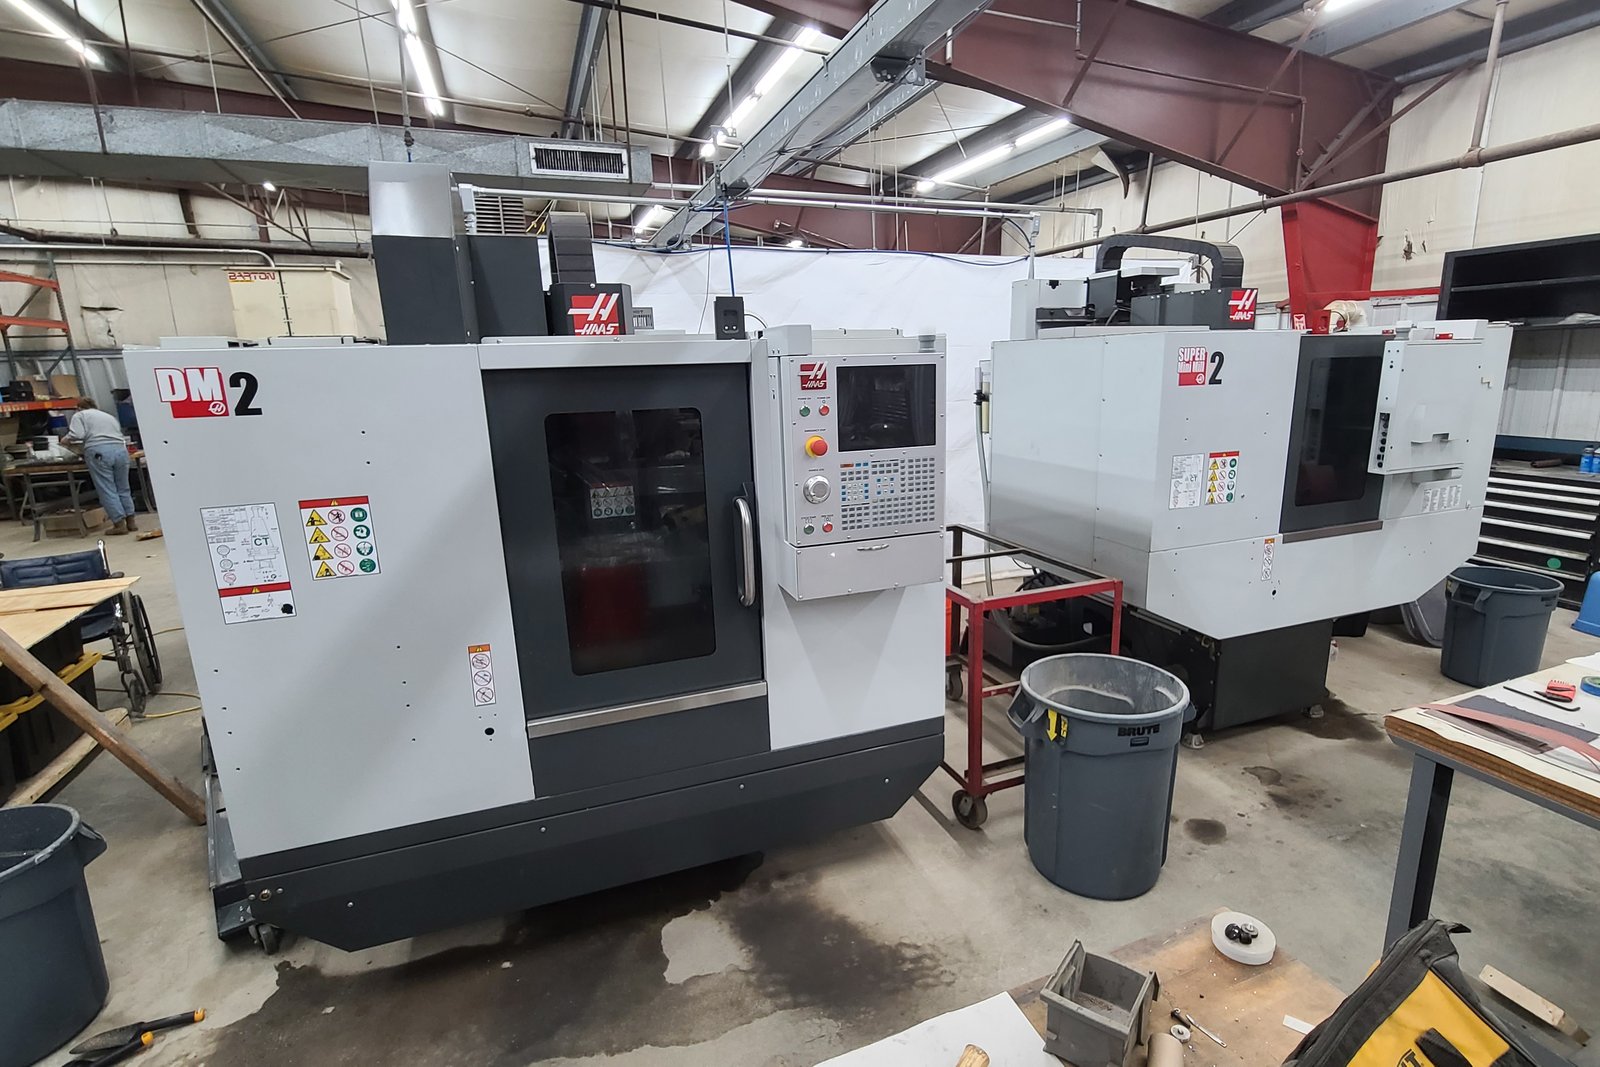
- Three-axis vertical machining centers, working envelope up to 28" × 16": counterbores, countersinks, chamfers, perimeter tooling, and custom inserts and fixtures
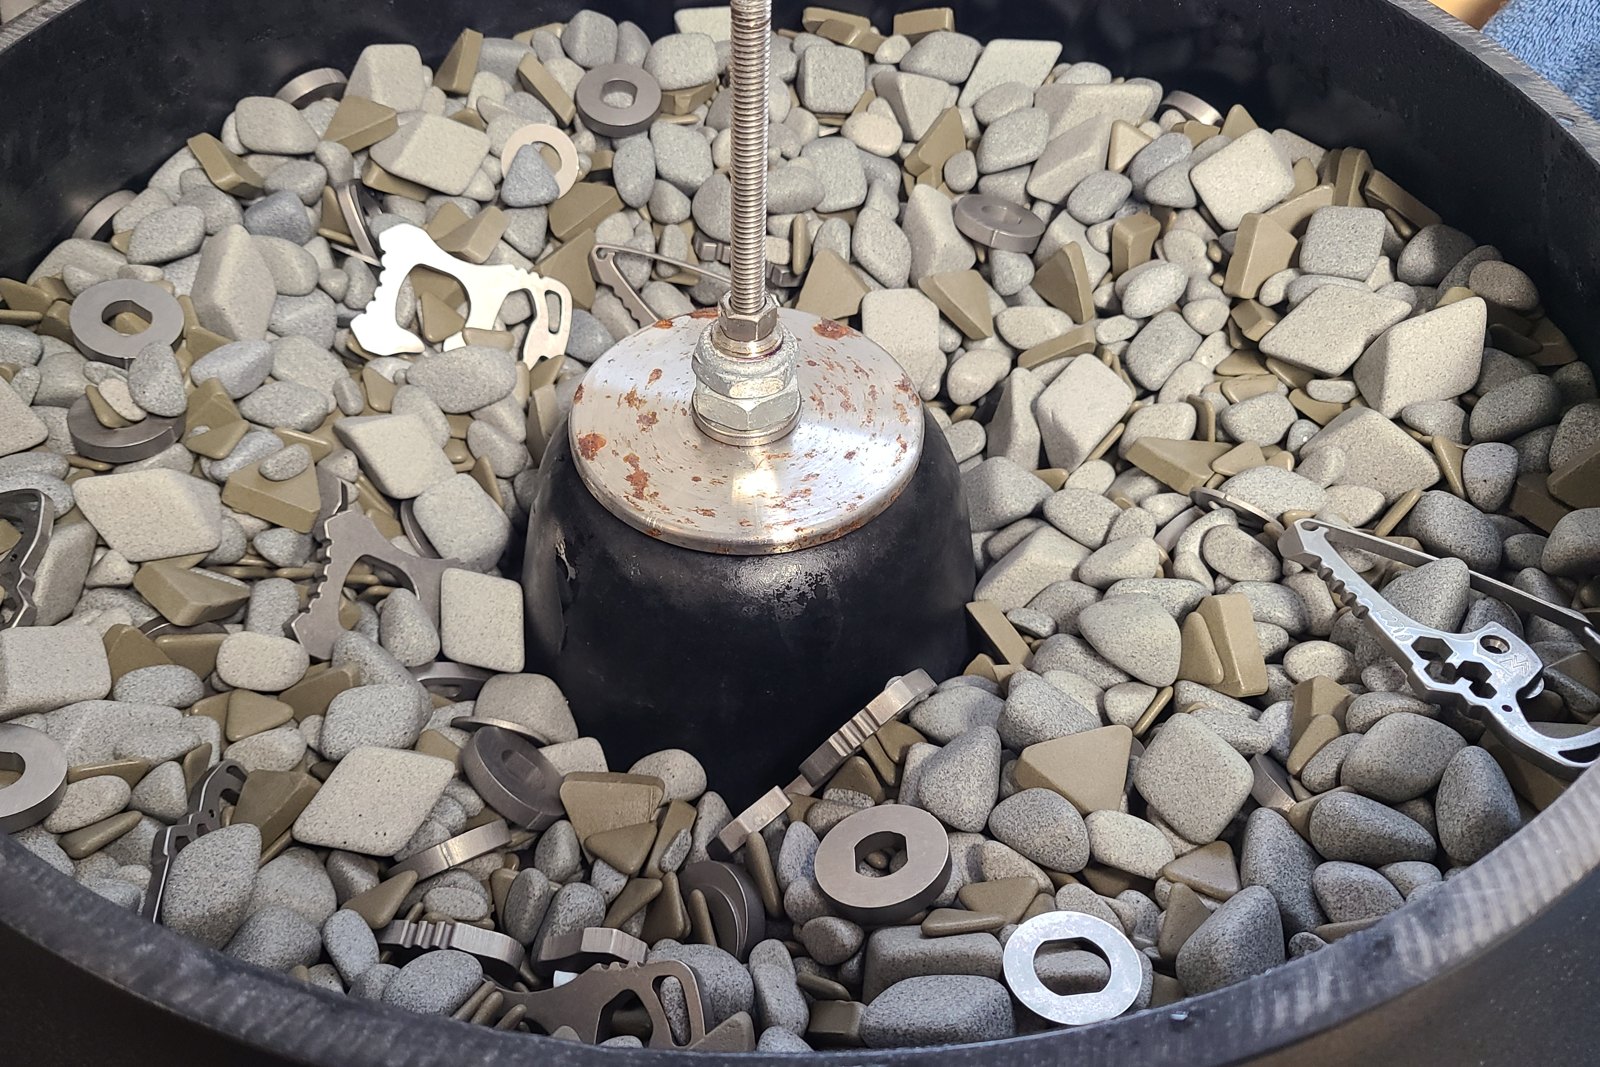
- Vibratory deburring: abrasive ceramic media with metered compound feed for corner rounding, deburring, and surface smoothing
- Vibratory polishing: plastic media for a soft polished finish
- Sandblasting, belt grinding, and buffing
- Hand finishing: polish, sanding, wire wheel, Scotch-Brite, stonewash, forced patina, and blackening
- Blade finishing and sharpening
Partner shops
We manage these for you: we ship to the partner and inspect before parts ship to you.
- Waterjet cutting
- Plasma cutting
- Laser cutting
- Surface grinding
- Bending and forming
- Heat treat
- Laser engraving and marking, including fill and etch
- Anodizing: solid, multicolor, and functional on titanium
- Type II color anodizing for aluminum
- Type III hard coat anodizing for aluminum
- Electropolish with passivation, for stainless steel, to a specified Ra on marked faces
- Cerakote
What we machine
Don’t know the right material for your application? We can help.
Below is a sample from the shop's job records since 2012, not a complete list. Sheet and plate from about 0.020" to 1" thick. Customer-supplied material is welcome, and leftover stock goes back to you.
| Material | Typical use |
|---|---|
| Titanium Grade 5 (6Al-4V) | EDC tools, pocket clips, knife hardware, lightweight structural parts |
| Titanium Grade 2 (CP) and Grade 38 | Grade 2 where formability matters more than strength; Grade 38 for the same uses as Grade 5 |
| Zirconium, Timascus, Moku-Ti | Premium and decorative pieces |
| Aluminum 6061-T651, 7075, 3003, 5052 | Machined brackets and parts (customer-supplied bar welcome), high-strength parts, sheet parts |
| Stainless 316/316L, 303, 301, 416 | Hygienic and sanitary parts (electropolished and passivated), machined parts, spring and sheet parts |
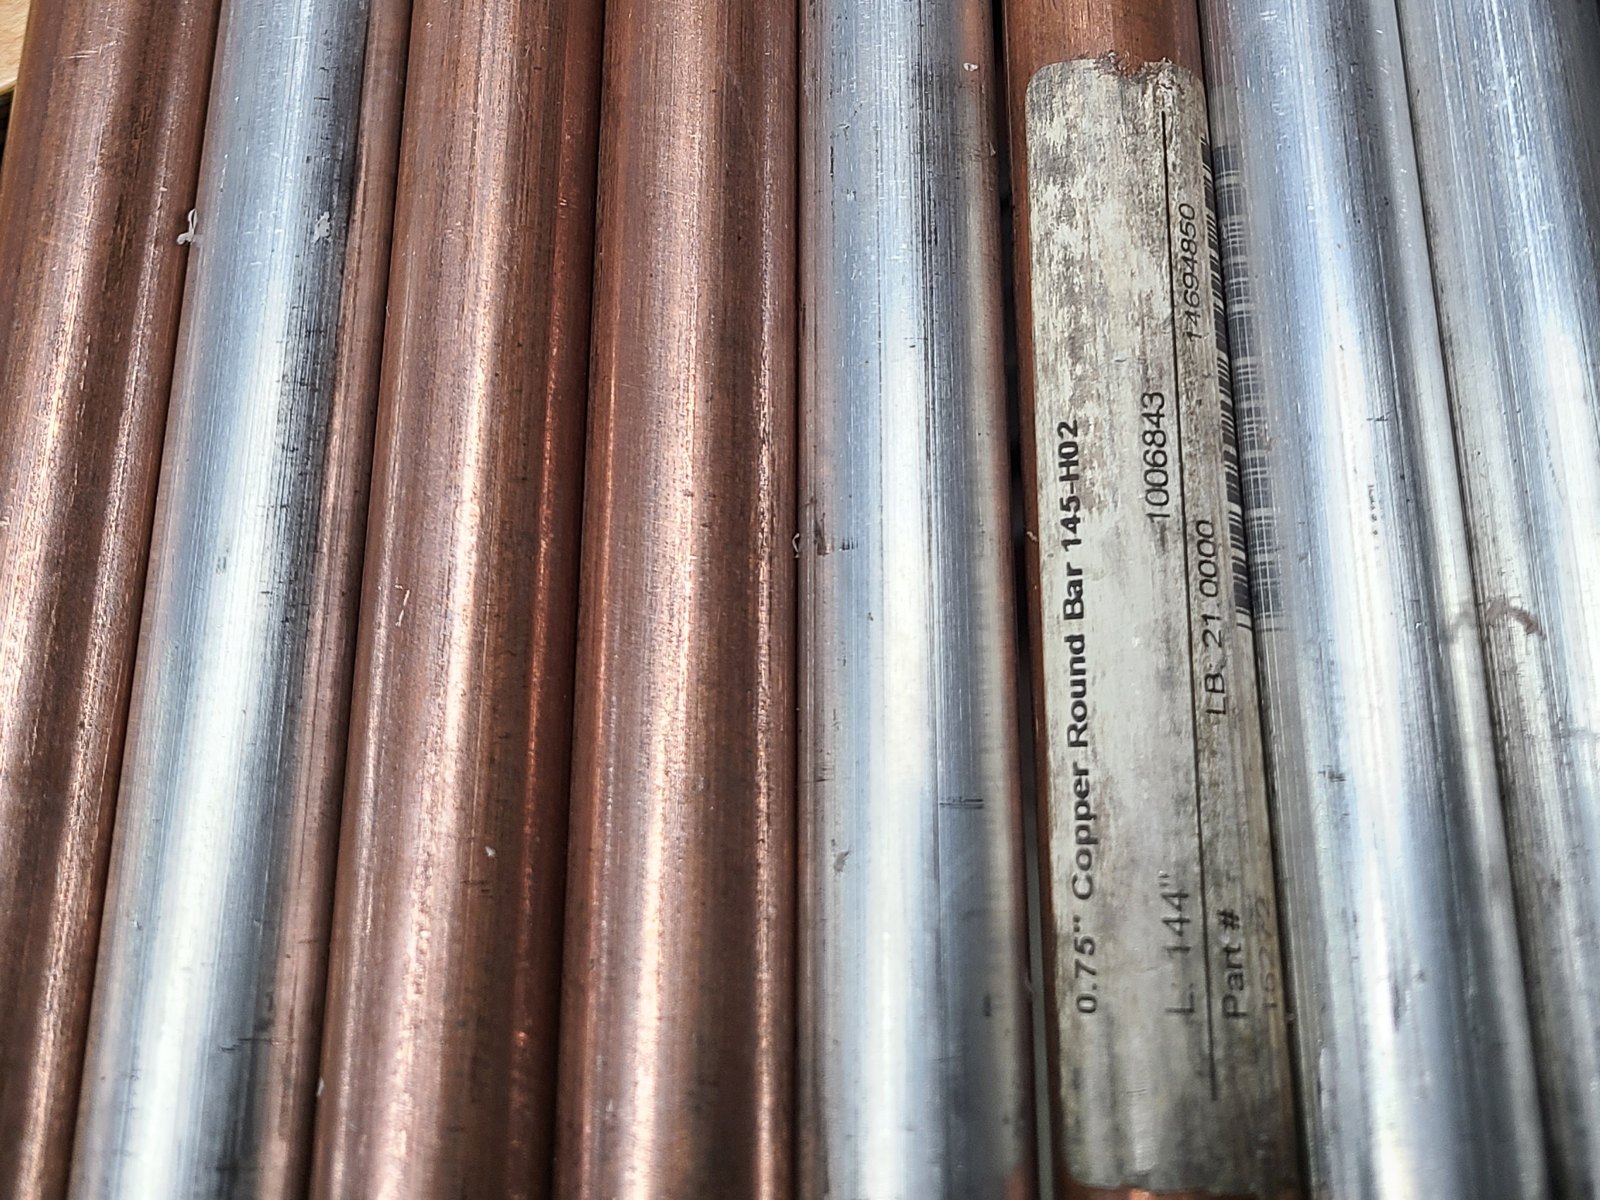
| Brass, copper (incl. tellurium copper), bronze, phosphor bronze, mokume | Hardware, decorative, and finish-critical parts |
| Knife and tool steels: MagnaCut, S35VN, S30V, CPM-154, AEB-L, 3V, D2, XHP, Elmax, Vanax, S90V, 1095, 52100, W1, Damascus | Knife blades |
| AR500, AR9000, A36 / mild steel | Wear parts, shooting targets, general parts |
| G10, Micarta, carbon fiber, Ultem (PEI), PETG / CF-PETG | Scales, insulators, light structural parts |
Quality and documents
- Material certs sent with the order, including extra original copies when the PO requires them
- Certificates of Conformance
- Inspection documents on request
- Customer drawings kept controlled in-house
- Quality records kept for 10 years
- No sub-tier outsourcing when your PO forbids it
Our own production, every week
SE Products restock runs
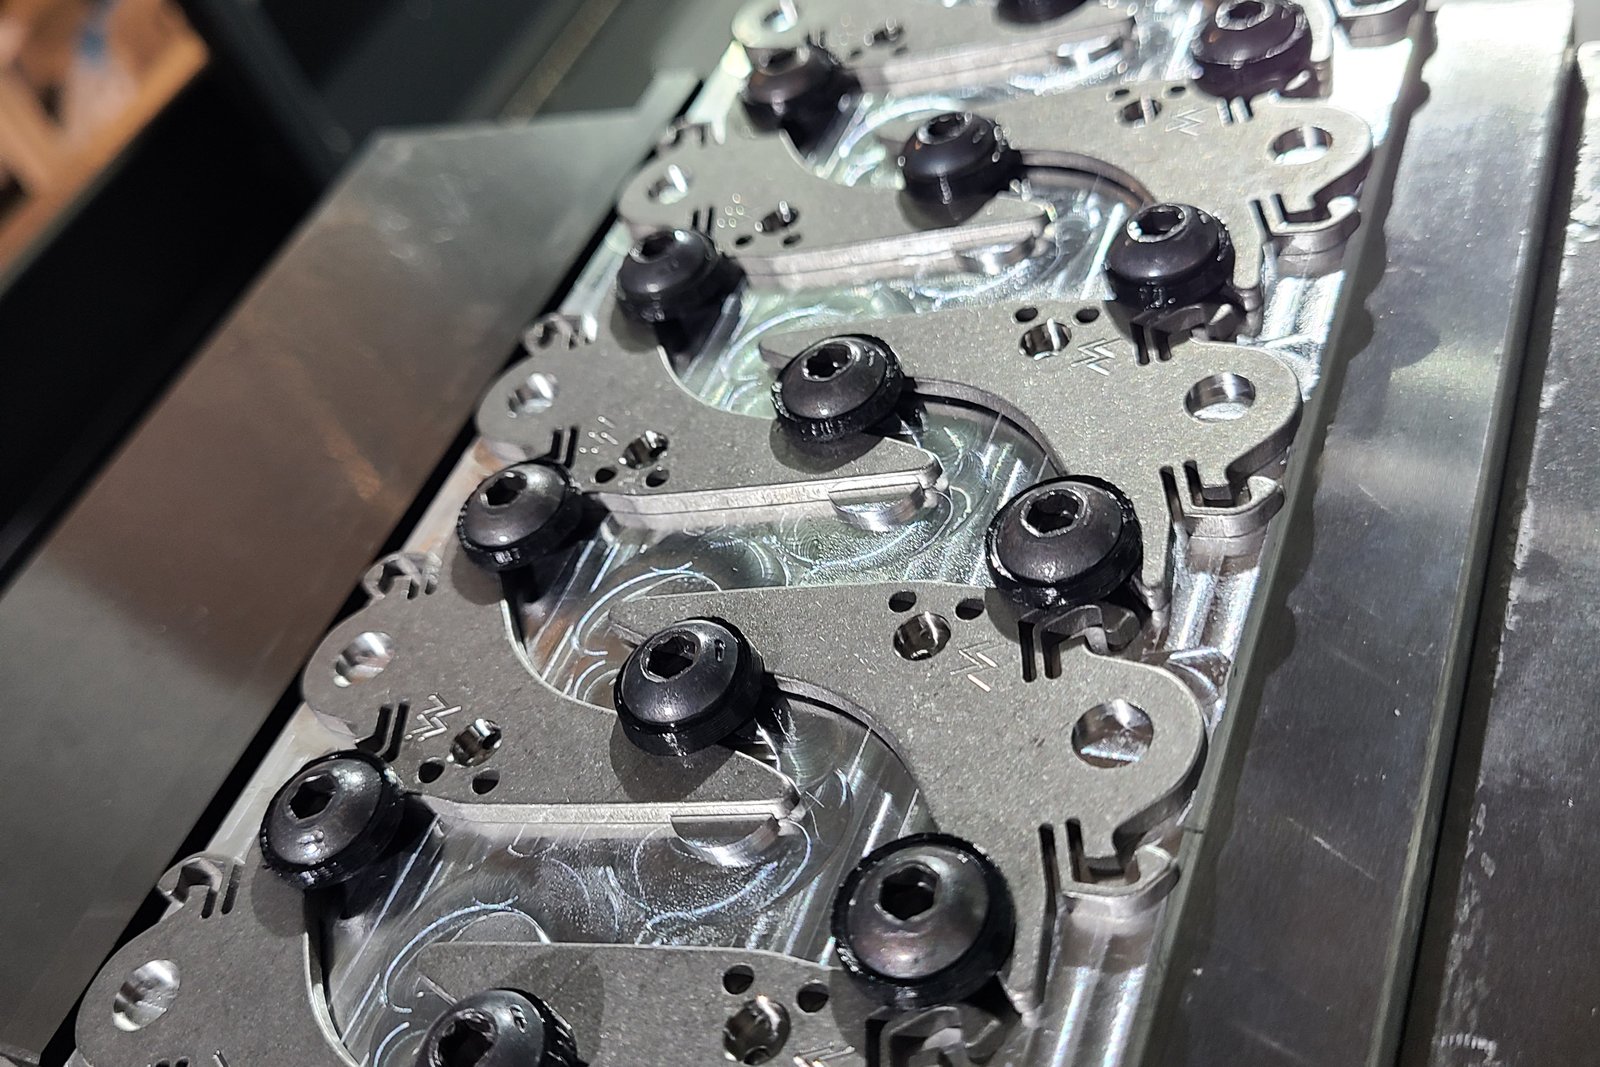
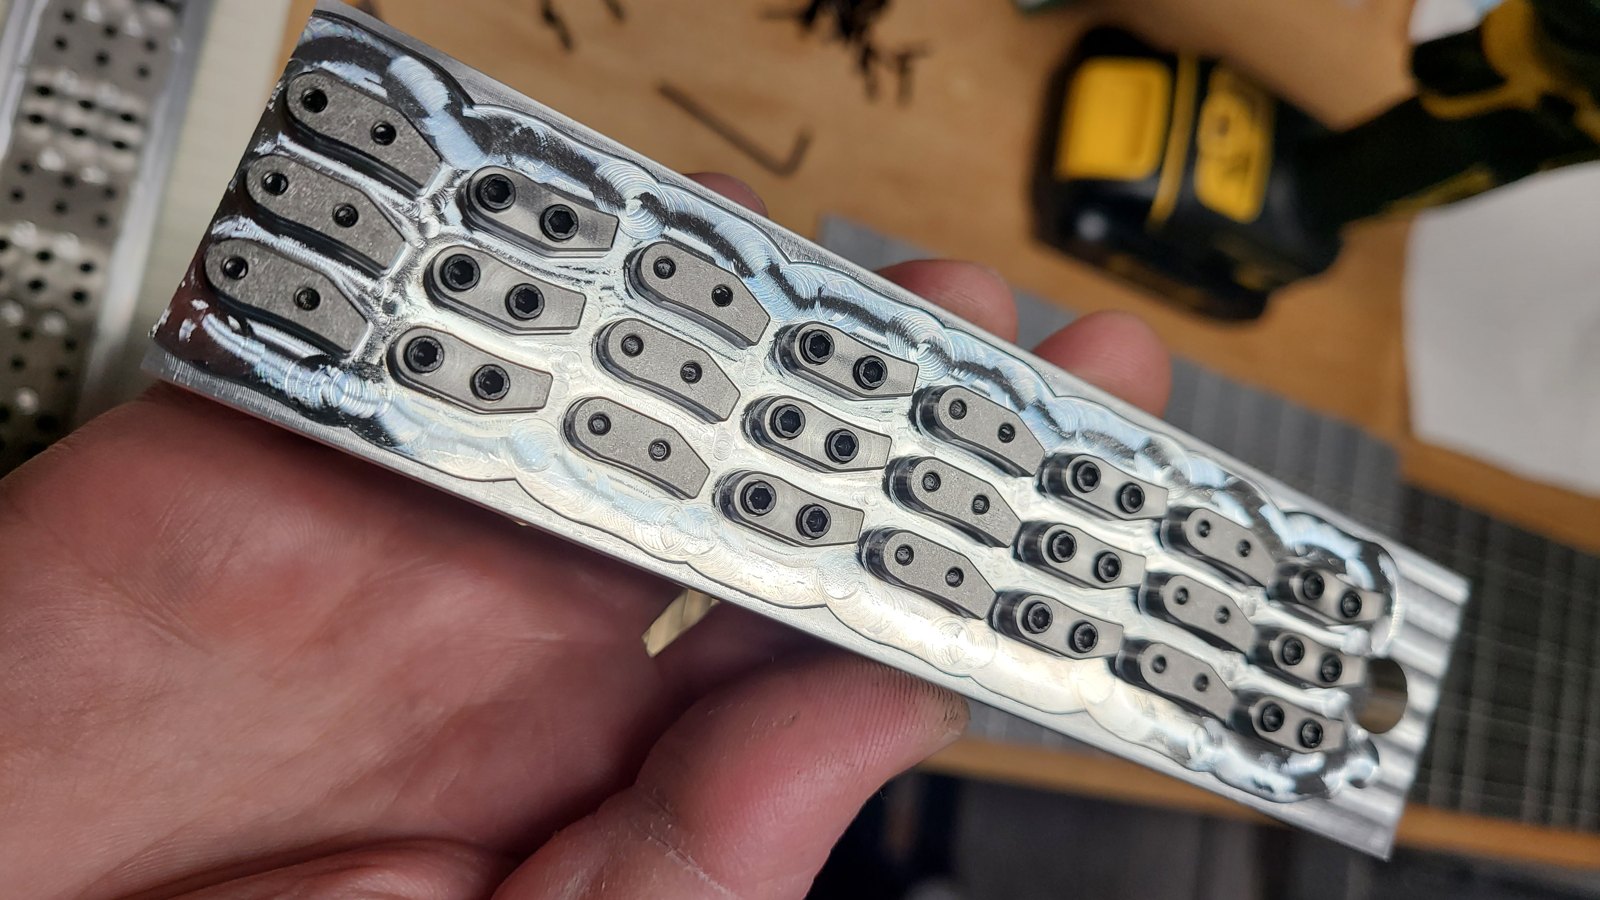
The Rook, C238, Utilizer, and HookUp Micro and Nano run through this shop in batches: Grade 5 titanium, machined on custom fixtures, tumbled in-house, and finished through the same partner chain we offer you. One Utilizer thumb-stud run meant 1,344 tiny 2-56 screws in and out of a fixture.
Manufacturing questions
What file types do you take?
STEP, IGES, or XT (Parasolid) for the 3D model, DXF for flat profiles, plus a PDF drawing with tolerances and finish callouts. We model in SolidWorks and program in Mastercam for SolidWorks. A 2D drawing, or even a napkin sketch, is fine too; see Product Design & Development.
What tolerances can you hold?
Tell us what the print needs and we will tell you plainly if we can hold it before we quote. If you’re interested in DFM feedback, just ask. Recent work includes counterbores held to +.002/-.000 and machined surfaces to 35 µin Ra, with faces finished to 15 to 20 µin Ra ahead of electropolish.
What is your lead time?
Lead times vary with the details of the job and how busy the shop is at the time, but most projects are completed within two to six weeks.
Is there a minimum order?
We have no minimum order quantity. Prototypes and small lots are normal here.
What finishes do you offer?
In-house: deburring, hard (ceramic) and soft (plastic) tumbling, stonewash, hand polish and satin finishes, and blackening. Through partner shops: bead blast, Zirblast, laser marking, titanium anodizing, hard anodizing for aluminum, electropolish with passivation, and Cerakote.
How do you ship?
Parts ship from Sellersville, PA, by USPS, UPS, or FedEx. We can bill shipping to your own FedEx or UPS account. Just include your account number and billing ZIP with your PO.
Send the drawing. Get a straight answer.
Send a drawing, a sketch, or just a description. The engineer who will make the part reads it first and comes back with questions or a quote.